 English
 中文


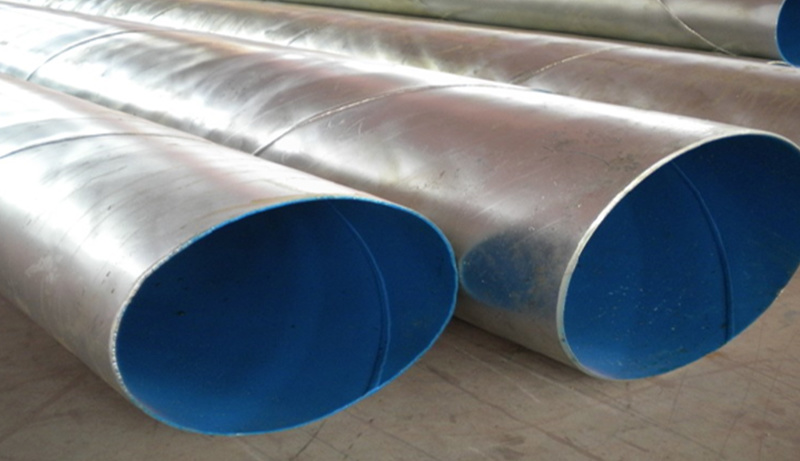
Zinc-plated pipe dedicated powder coating
- Commodity name: Zinc-plated pipe dedicated powder coating
- Product Description
-
Product Features1. Excellent adhesion to steel pipe substrates, with adhesion reaching level 2.2. The coating surface has good leveling and high gloss, high surface hardness, and high coating density.3. It has extremely strong anti-permeability and anti-corrosion capabilities, and can withstand the erosion and scouring of medium and high-temperature water and steam for a long time.4. The coating has excellent high-temperature cathodic delamination resistance.5. Good mechanical properties, strong flexibility, greatly improving the defect of poor adhesion of ordinary powder on the galvanized layer.6. Good powder fluidity, large spraying area, effectively reducing dust pollution during spraying.Epoxy Powder Performance Parameters
Item
Quality Index
Test Method
Test Results
Appearance
Uniform color, no agglomeration
Visual GB/T 1729-1979
Qualified
Density (g/cm³)
1.3-1.5
GB/T 4472
1.45±0.03
Non-volatile content (%)
≥99.5
GB/T 6554
99.90%
Spraying area
\
Film thickness 300μm
2.29-2.39m²/kg
Horizontal fluidity/mm
22-28
GB/T6554-2003
26
Gelation time (200℃)
≤120s
GB/T6554-2003
100±5s
Impact strength/(KG*CM)
≥50
GB/T1732-1986
50
Cured Powder Coating Performance ParametersSerial Number
Test Item
Technical Index
Test Method
Test Results
1
Appearance
Uniform color, no bubbles, no cracks or shrinkage, slight orange peel is allowed
Visual inspection
GB/T 1729-1979Qualified
2
Adhesion (grade)
1~3
GB/T 28897-2012
Grade 2
3
Impact resistance
No peeling, no cracking
GB/T 28897-2012
Qualified
4
Bending test
No peeling, no cracking
GB/T 28897-2012
Qualified
5
Flattening test
No cracks, no breaks
GB/T 28897-2012
Qualified
6
Volume resistivity (Ω.m)
≥1×10¹³
GB/T1410
1.8×10¹⁴
7
Dielectric strength (MV/m)
≥30
GB/T1408
38.5
8
Pinhole test
No electric sparks
GB/T 28897-2012
Qualified
9
Warm water aging test
No peeling or cracking of the coating
GB/T 28897-2012
Qualified
10
Anti-aging performance
Gloss retention above 80%, color difference ≤2.0, no powdering or chalking of the coating
GBT1865-1997
Qualified
11
High temperature resistance
Darkening of the color is allowed, but the coating should be free of peeling, blistering, cracking, delamination, or damage
GB/T 28897-2012
Qualified
12
Low temperature resistance
The coating should be free of peeling or damage; the adhesion test should be grade 1-3
GB/T 28897-2012
No change in coating, adhesion grade 2
13
Cup test (mm)
≥2
GB/T9753-88
3
14
Temperature cycle test
The coating should be free of peeling or damage; the adhesion test should be grade 1-3
GB/T 28897-2012
No change in coating, adhesion grade 2
Applicable processes: Electrostatic spraying, dipping, rolling, etc.Precautions:1. The surface of the steel pipe should be free of oil stains, loose rust, and moisture; the surface treatment quality should reach Sa2 1/2 grade (GB/T8923); the anchor pattern depth should be 50-90mm; dust and abrasives attached to the surface of the steel pipe should be blown clean; preheating: the surface temperature of the steel pipe should be controlled at 160-200℃, and should not exceed 230℃.Unused powder should be stored indoors in a well-ventilated, dry area with a temperature below 40℃, away from heat sources, corrosive chemicals, and chemical solvents. Avoid direct sunlight; the maximum stacking height should not exceed 4 layers; avoid prolonged compression, ensure the packaging box is sealed to prevent caking and moisture, affecting the coating performance.To maximize the corrosion protection of the epoxy coating, the coated steel pipes need to undergo secondary heat curing.
Product consultation
If you are interested in our products, please leave us a message!
Hot products

Scan the QR code
Contact us
Address: Qichun County, Huanggang City, Hubei Province, China
Li Shizhen Industrial Park, North Huan Road
Tel: 86-13801790539 (Mr. Luo)
Email: tedluo@163.com